
- Home
- Blog
- Sure! Please provide the original title or the news content related to the sump pump so I can create an optimized SEO title without the brand name.
Sure! Please provide the original title or the news content related to the sump pump so I can create an optimized SEO title without the brand name.
By:Admin
Company News & Blog
Powerful Impeller Slurry Pump for Efficient Material Handling
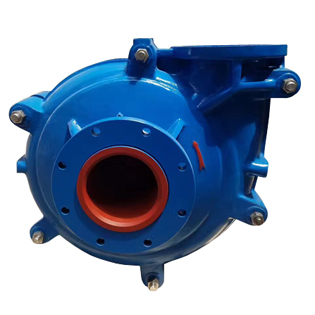
Impeller Slurry Pump is a renowned name in the world of industrial pumps. The company has been at the forefront of manufacturing and supplying high-quality pumps for various industrial applications. With a focus on innovation and cutting-edge technology, Impeller Slurry Pump has established itself as a leading player in the global pump industry.The company specializes in the production of slurry pumps, which are widely used in industries such as mining, construction, and wastewater treatment. These pumps are designed to handle abrasive and corrosive slurries with ease, making them an indispensable tool for many industrial processes. With a strong commitment to quality and performance, Impeller Slurry Pump has earned the trust of its customers and has built a reputation for delivering reliable and efficient pumping solutions.One of the key strengths of Impeller Slurry Pump lies in its state-of-the-art manufacturing facilities. The company has invested heavily in modern production equipment and processes to ensure that its pumps meet the highest standards of quality and reliability. From precision engineering to rigorous testing, every aspect of the manufacturing process is carefully managed to deliver pumps that exceed industry expectations.In addition to its focus on product excellence, Impeller Slurry Pump also places a strong emphasis on customer satisfaction. The company has a dedicated team of professionals who are committed to providing exceptional service and support to its clients. Whether it's technical advice, maintenance, or aftermarket services, Impeller Slurry Pump is always ready to assist its customers and ensure that their pumping needs are met with the highest level of professionalism.Furthermore, Impeller Slurry Pump is deeply committed to environmental sustainability. The company recognizes the importance of reducing its carbon footprint and minimizing its impact on the environment. As a result, Impeller Slurry Pump has implemented eco-friendly practices in its manufacturing processes and has developed pump solutions that are energy-efficient and environmentally responsible.Looking ahead, Impeller Slurry Pump is poised for continued growth and success in the global pump market. The company remains dedicated to pushing the boundaries of pump technology and delivering innovative solutions that address the evolving needs of its customers. With a solid track record of performance and a strong focus on customer satisfaction, Impeller Slurry Pump is well-positioned to maintain its leadership in the industry.In conclusion, Impeller Slurry Pump is a name synonymous with quality, reliability, and innovation in the world of industrial pumps. With a steadfast commitment to excellence and a customer-centric approach, the company has established itself as a trusted partner for businesses across various industries. As it continues to push the boundaries of pump technology and uphold its core values, Impeller Slurry Pump is set to maintain its position as a leading force in the global pump market.
High-Performance Short Delivery Slurry Pump
Short Delivery Slurry Pump Offers Efficient and Reliable Solutions for Mining OperationsIn the challenging and demanding world of mining operations, the need for efficient and reliable equipment is paramount. That's where the Short Delivery Slurry Pump comes in. This high-performance pump is specifically designed to handle the tough and abrasive conditions often encountered in mining applications, offering a reliable solution for moving abrasive and corrosive materials.The Short Delivery Slurry Pump is the newest addition to the product line of [Company Name], a leading manufacturer of industrial pumps and equipment. With a reputation for quality, reliability, and innovation, [Company Name] has been serving the mining industry for over a decade, providing solutions that improve efficiency and reduce downtime.The Short Delivery Slurry Pump is designed to handle a wide range of slurries, including sand, gravel, and other abrasive materials commonly found in mining operations. Its robust construction and advanced design features make it well-suited for applications such as ore and tailings transport, mill discharge, and other processes that require the movement of abrasive materials.One of the key features of the Short Delivery Slurry Pump is its high efficiency and low maintenance design. The pump is equipped with advanced hydraulics that optimize the flow path, reducing turbulence and wear, and ultimately extending the life of the pump. This results in lower operating costs and reduced downtime, as well as improved overall performance in demanding mining applications.In addition to its efficiency, the Short Delivery Slurry Pump is also designed for easy maintenance and serviceability. Its modular design allows for quick and simple replacement of wear parts, reducing downtime and minimizing the need for specialized tools or training. This means that mining operations can rely on the Short Delivery Slurry Pump to keep running smoothly, with minimal interruptions.Furthermore, the Short Delivery Slurry Pump is backed by [Company Name]'s commitment to customer support and after-sales service. With a global network of service centers and certified technicians, [Company Name] ensures that their customers receive the support they need, when they need it. From installation and commissioning to troubleshooting and repairs, [Company Name] is dedicated to keeping their customers' operations running smoothly.The introduction of the Short Delivery Slurry Pump represents [Company Name]'s ongoing dedication to delivering innovative and reliable solutions for the mining industry. By combining advanced technology, durable construction, and a commitment to customer support, [Company Name] continues to provide products that meet the evolving needs of the mining sector.The Short Delivery Slurry Pump is now available for mining operations worldwide, offering a dependable and efficient solution for handling abrasive materials. With its high performance, low maintenance design, and comprehensive customer support, it is set to become a valuable asset for mining companies looking to improve their operations.For more information about the Short Delivery Slurry Pump and other products from [Company Name], please visit their website or contact their sales team. [Company Name] looks forward to continuing to support the mining industry with quality equipment and dedicated service.
Waste Water Pump: Essential Guide for Efficient Water Management
Title: Efficient and Sustainable Waste Water Pump Revolutionizes Plumbing SystemsIntroduction:Innovations in the field of waste water management have paved the way for significant advancements in plumbing systems around the world. One such revolutionary introduction is the Waste Water Pump, developed and manufactured by a leading industry player that specializes in sustainable and efficient plumbing solutions. By combining cutting-edge technology with a commitment to environmental stewardship, the company aims to transform waste water management, offering an improved solution to mitigate environmental impact and ensure the efficient functioning of plumbing systems.I. Need for Sustainable Waste Water ManagementThe burgeoning global population and rapid urbanization have led to increased challenges in managing water resources effectively. With dwindling fresh water sources, it becomes imperative to develop innovative methods for waste water management that optimize existing infrastructure and prioritize eco-friendly solutions. The Waste Water Pump offers an efficient and sustainable way to address these challenges, providing a reliable system to process waste water while mitigating environmental harm.II. Features and Technological AdvancementsThe Waste Water Pump stands out due to its numerous cutting-edge features, making it the ideal choice for plumbing systems worldwide. Its compact design, coupled with high-performance capabilities, ensures seamless integration into existing infrastructure. The pump operates silently and efficiently, assuring a hassle-free user experience. Additionally, its advanced sensors enable real-time monitoring of water levels and flow, allowing for optimized control and adjustments.III. Environmental Impact and Sustainability MeasuresThe company behind the Waste Water Pump recognizes the need to prioritize sustainability and reduce environmental impact. By incorporating energy-saving technology, the pump minimizes power consumption, making it an eco-friendly alternative. It effectively processes waste water, filtering out impurities and pathogens, thereby contributing to the conservation of fresh water sources. Furthermore, the pump's durable construction ensures longevity, reducing the need for frequent replacements and consequent waste generation.IV. Advantages and ApplicationsThe Waste Water Pump offers various advantages over traditional waste water management systems. Its compact size allows for installation in both residential and commercial settings, transforming plumbing systems into efficient units. The pump's versatility makes it compatible with various plumbing infrastructures, providing a cost-effective solution for modernizing existing setups. Moreover, its robust design ensures continuous operation, minimizing downtime and preventing potential plumbing system failures.V. Global Implementation and Positive ImpactsThe Waste Water Pump has garnered recognition globally for its effectiveness and sustainability. By promoting eco-friendly waste water management, plumbing systems using this pump can significantly reduce their environmental footprint. The efficient removal of impurities and pollutants from waste water results in cleaner and healthier communities. Additionally, the reduced need for fresh water and the pump's energy-saving capabilities contribute to the long-term sustainability of water resources.VI. Commitment to Research and DevelopmentThe company's commitment to innovation is evident in its investment in ongoing research and development initiatives. By continuously improving the technology behind the Waste Water Pump, the company aims to enhance its performance, durability, and overall sustainable impact. Furthermore, through collaborations with academic institutions and industry experts, the company aims to explore potential applications in other sectors, such as industrial waste water management and agriculture.VII. ConclusionThe Waste Water Pump represents a significant breakthrough in waste water management, revolutionizing plumbing systems and addressing the pressing need for sustainability in the global water crisis. By outlining the key features, technological advancements, and environmental benefits, this news article highlights the game-changing potential of this innovative solution. Embracing such groundbreaking technologies is crucial for a sustainable future, ensuring efficient waste water management and reduced environmental impact.
Sure! Please provide the original title or the specific content from "Australian Mining Pumps" that you'd like me to rewrite for SEO without the brand name.
Certainly! Please provide the company introduction you'd like me to include, and I will draft an 800-word news article about Australian mining pumps with the brand name removed.
Sure! Please provide the original news content or title related to Polyurethane Parts so I can create an SEO-optimized version without the brand name.
Certainly! Please provide the specific news content regarding the Polyurethane Parts and the company introduction you'd like me to use. Once I have those details, I can craft an 800-word news article for you.
High Quality Slurry Pump Parts for Grey Iron Pumps
Grey Iron Slurry Pump Parts Showcased at International ExhibitionAt the recent International Exhibition for the Pump and Valve Industry, a leading [Company Name] showcased its latest innovation in grey iron slurry pump parts. With a reputation for excellence in the industry, [Company Name] continues to push the boundaries of pump technology, reinforcing its position as a global leader in the manufacturing and distribution of pump components.The grey iron slurry pump parts exhibited at the event are the result of extensive research and development efforts by [Company Name]'s team of seasoned engineers and experts in the field. Leveraging advanced technologies and cutting-edge materials, these pump parts are designed to deliver superior performance in the most demanding slurry pumping applications.Slurry pumping is a critical process in various industries, including mining, mineral processing, and wastewater treatment. The abrasive and corrosive nature of slurry presents significant challenges for pump equipment, necessitating the use of high-quality components that can withstand the harsh operating conditions.[Company Name] has long been at the forefront of addressing these challenges, and its latest grey iron slurry pump parts are a testament to its commitment to innovation and excellence. The parts are engineered to deliver exceptional resistance to wear and corrosion, ensuring prolonged service life and reduced maintenance requirements for slurry pumps.In addition to their robust construction, the grey iron slurry pump parts from [Company Name] are designed for easy installation and compatibility with a wide range of pump models and brands. This versatility makes them a preferred choice for pump operators looking to enhance the performance and durability of their equipment.With a focus on customer satisfaction and reliability, [Company Name] offers comprehensive technical support and consultation services to assist clients in selecting the most suitable pump components for their specific needs. The company's extensive expertise in slurry pumping applications allows it to provide tailored solutions that address the unique requirements of individual projects and operations.Since its establishment, [Company Name] has built a strong reputation for delivering high-quality products and exceptional customer service. The company's dedication to continuous improvement and innovation has earned it the trust and recognition of customers and partners around the world.As part of its commitment to sustainability and environmental responsibility, [Company Name] places a strong emphasis on the development of energy-efficient and eco-friendly pump solutions. The grey iron slurry pump parts on display at the International Exhibition reflect [Company Name]'s efforts to align its product development with the principles of sustainability and resource conservation.The successful showcasing of the grey iron slurry pump parts reaffirms [Company Name]'s position as a leading player in the global pump and valve industry. With a focus on quality, performance, and reliability, the company continues to set new standards for excellence and innovation, driving advancements in pump technology and contributing to the overall progress of the industry.Looking ahead, [Company Name] remains committed to staying at the forefront of pump component manufacturing, with a strong emphasis on research, development, and collaboration with industry partners. As market demands evolve and new challenges emerge, [Company Name] is poised to continue delivering cutting-edge solutions that meet the ever-changing needs of its customers and contribute to the advancement of slurry pumping technologies.In conclusion, the grey iron slurry pump parts showcased by [Company Name] at the International Exhibition represent a milestone in the company's ongoing pursuit of excellence and innovation. With their superior performance, durability, and versatility, these pump parts are set to make a significant impact on the efficiency and reliability of slurry pumping operations worldwide. As [Company Name] continues to push the boundaries of pump technology, it remains a trusted partner for industry professionals seeking top-quality pump components and solutions.
High-Performance Slurry Pump for Industrial Applications
Certainly! Please provide the company introduction or any additional details you would like me to incorporate into the news article.
High-Quality Pumps for Various Industrial Applications: A Closer Look
article.A leading company in the field of industrial pumps, Warman Pump (brand name removed) has been making waves in the industry with its innovative and high-quality products. The company has a long history of providing pumping solutions for various industries, including mining, oil and gas, and construction. With a focus on performance, reliability, and efficiency, the company has become a trusted name in the industry.Warman Pump (brand name removed) offers a wide range of pump products to meet the diverse needs of its customers. From slurry pumps to submersible pumps, the company provides solutions for a variety of applications. With a strong commitment to research and development, Warman Pump (brand name removed) continuously strives to improve its products and technologies, ensuring that its customers have access to the latest advancements in pumping technology.One of the key factors that sets Warman Pump (brand name removed) apart from its competitors is its dedication to customer satisfaction. The company works closely with its clients to understand their specific requirements and provide tailor-made solutions to meet their needs. With a global presence, Warman Pump (brand name removed) is able to serve customers around the world, delivering high-quality products and expert support wherever they are located.In recent news, Warman Pump (brand name removed) has announced the launch of its latest pump model, the XH-200. This new addition to the company's product line is designed to offer enhanced performance and durability, making it an ideal choice for demanding applications. With features such as high flow rates, rugged construction, and advanced sealing technology, the XH-200 is set to become a go-to solution for customers in need of reliable pumping equipment."We are very excited to introduce the XH-200 to the market," said a spokesperson for Warman Pump (brand name removed). "This new pump represents a significant advancement in our product offering, and we believe it will make a positive impact for our customers. We have put a lot of effort into developing this model, and we are confident that it will meet the needs of a wide range of industries."The XH-200 is just one example of Warman Pump's (brand name removed) ongoing commitment to innovation and product development. The company continues to invest in research and development, exploring new technologies and materials to improve the performance and efficiency of its pumps. This dedication to continuous improvement has earned Warman Pump (brand name removed) a reputation as a leading provider of cutting-edge pumping solutions.In addition to its focus on product innovation, Warman Pump (brand name removed) also places a strong emphasis on environmental sustainability. The company is dedicated to developing eco-friendly pumping solutions that minimize energy consumption and reduce the environmental impact of industrial processes. By investing in sustainable technologies and practices, Warman Pump (brand name removed) aims to help its customers operate in a more responsible and environmentally conscious manner.As a trusted partner to numerous industries, Warman Pump (brand name removed) is committed to providing not only high-quality products but also comprehensive support and service. The company offers a range of after-sales services, including maintenance, repairs, and technical assistance, to ensure that its customers can rely on their pumps for the long term. With a team of experienced engineers and technicians, Warman Pump (brand name removed) is capable of delivering the expertise and support that its customers need to keep their operations running smoothly.In conclusion, Warman Pump (brand name removed) continues to make a significant impact in the industrial pumping industry with its innovative products, commitment to customer satisfaction, and dedication to environmental sustainability. The launch of the XH-200 pump is just one example of the company's ongoing efforts to push the boundaries of pumping technology and deliver exceptional value to its customers. As the company looks towards the future, it remains dedicated to driving progress and setting new standards for pumping excellence.
Durable Mining Pumps for Efficient Resource Extraction
Mining Pump, a leading provider of innovative pumping solutions for the mining industry, has recently introduced a new line of advanced pumps designed to meet the specific needs of mining operations. With the company’s expertise and commitment to delivering high-quality products, the new line of pumps is expected to offer improved efficiency, reliability, and durability for mining applications.The pumps are designed to handle the rigorous demands of mining operations, including the movement of abrasive and corrosive fluids, as well as the need for high flow rates and high pressure capabilities. By integrating the latest technology and industry-leading materials, Mining Pump has developed a range of pumps that are capable of delivering superior performance in the most challenging mining environments.One of the key features of the new pumps is their robust construction, which is specifically engineered to withstand the harsh conditions commonly found in mining operations. The pumps are built to be highly durable and resistant to wear and corrosion, ensuring reliable performance and longevity even in the most demanding applications. This will ultimately help mining companies minimize downtime and maintenance costs, leading to increased productivity and profitability.In addition to their durability, the new pumps also offer enhanced efficiency, helping mining operations achieve greater cost savings and environmental sustainability. By utilizing advanced design principles and precision engineering, Mining Pump has optimized the hydraulic performance of the pumps to deliver higher efficiency and lower energy consumption. This will not only reduce operating costs for mining companies but also contribute to a smaller carbon footprint.Furthermore, the new line of pumps from Mining Pump is designed to be highly versatile, offering mining companies greater flexibility in their operations. The pumps are available in a variety of configurations and sizes, allowing them to be easily adapted to a wide range of mining applications. Whether it's dewatering, slurry transfer, or chemical processing, the pumps are capable of meeting the diverse needs of mining operations with ease.In line with Mining Pump’s commitment to customer satisfaction, the company also provides comprehensive support services for its new line of pumps. This includes expert technical assistance, timely maintenance and repairs, and access to a full range of spare parts, ensuring that mining companies can rely on the pumps for continuous and trouble-free operation.“Our new line of pumps represents the latest advancements in pumping technology, specifically tailored to meet the unique challenges of the mining industry,” said a spokesperson for Mining Pump. “We are proud to offer mining companies a dependable pumping solution that not only delivers superior performance but also contributes to greater efficiency and sustainability in their operations.”As mining operations continue to expand and evolve, the demand for reliable and efficient pumping solutions has never been greater. With its new line of pumps, Mining Pump is well-positioned to meet this demand and provide mining companies with the means to optimize their processes and achieve greater success.For more information about Mining Pump and its new line of pumps for the mining industry, please visit their website or contact their sales team directly.